Common Problems and Solutions of Die Casting Die
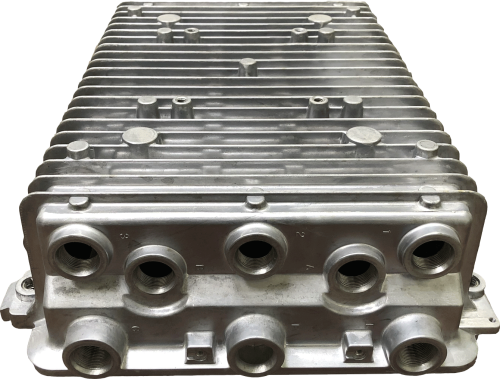
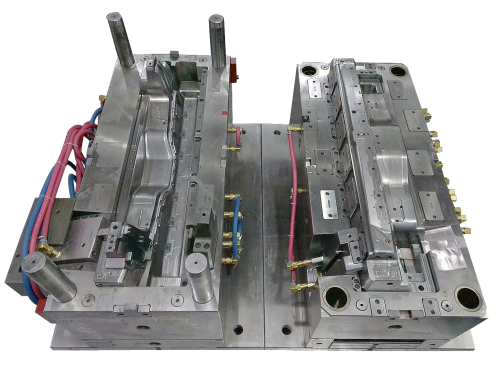
Die-casting die is a method of casting liquid forging. The surface temperature of die-casting die is very important to the quality of products. If the temperature is not well controlled, it will lead to deformation, size instability, and even surface depression, hot bubbles, shrinkage holes and other defects. In the process of die casting die, there will be some problems. Today, Shenzhen Zhongxin Tongtai Technology Co., Ltd. will introduce the common problems and solutions of lower die casting die.
1. Shrinkage cavity
Reason: In the process of die casting die, when the metal is changed from liquid to solid, shrinkage will occur if the metal is not replenished in time because of its shrinkage, which usually occurs in the place where solidification is slower. The solutions are: increasing pressure, changing the temperature of die casting die, cooling the die locally, and lowering the die temperature. Sometimes it is to change the position of shrinkage holes rather than eliminate them.
2. Stomata
The reasons are as follows: when the gas is dissolved, it is produced in the release agent, the material pipe and the mould; one is that air is mixed in the molten soup. The solutions are: slowing down the speed; using vacuum; checking whether the turning of the runner is smooth and the cross-section area has been gradually reduced; whether the die temperature is too low; whether the airway is blocked or not, whether the area is large enough, and so on. Correct treatment is carried out according to the test results.
3. Holes on the parting face:
Cause: It may be stomata or shrinkage.
Solutions are: cooling gate; if it is air hole, attention should be paid to the problem of entrainment and exhaust; if it is shrinkage hole, the thickness of overflow well inlet or gate should be reduced, which is a common problem encountered by die casting die.
Cause: Because of the sudden decrease of pressure, the gas in the molten soup suddenly expands and impacts the mould, resulting in the damage of the mould.
The solution is that the cross-section area of the runner must not change dramatically.
Above introduced the common problems and solutions of die-casting die, we have a certain understanding, in the process of die-casting die, if you encounter the above problems, you can refer to the above content to solve, or ask professional maintenance personnel to deal with. If there are any questions or doubts about die casting die, you can contact Shenzhen Zhongxin Tongtai Technology Co., Ltd.