Common Faults and Solutions of Injection Mold
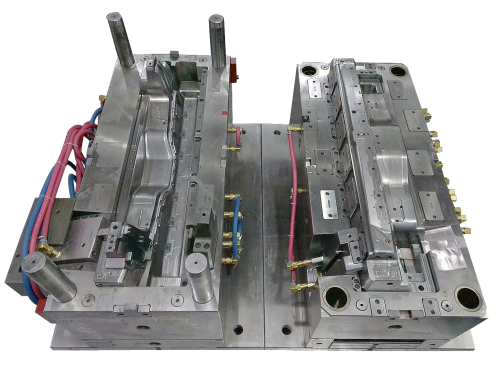
Injection mould is not only a tool for producing plastic products, but also a tool for making plastic products have complete structure and precise size. This tool makes the injection process rigorous and serious. Mould unconsciously cooperates with many basic work to achieve the completion of plastic products. The process of injection moulding contains a lot of basic elements that need to be coordinated, so no slip is allowed. Inevitably, the long-term use of the mold is bound to have such or such problems, then in the injection mold production and plastic products production practice, the most common injection mold failure causes and solutions?
The guide pillar is mainly the guiding function, which is used to ensure that the forming surfaces of the core and the cavity do not touch each other under any circumstances. The guide pillar was damaged. In any case, the guide pillar should not be used as a force member or positioner.
In the following two cases, when the injection is moving, the fixing of the die will produce a huge lateral offset force:
(1) When the wall thickness of plastic parts is not uniform, the material flow rate through the thick wall is high, which produces greater pressure, causing unnecessary trouble.
(2) The side of the plastic part is asymmetrical, such as the back pressure on the opposite side of the stepped parting surface. These may lead to unexpected results. The function of the guide pillar can exert its effect. That's the best thing.
In some cases, due to the limitation of template area, the length of guide groove is too small, which causes the slider to expose outside the guide groove after core-pulling operation. It is difficult to maintain the slider. In this way, it is easy to cause the slider to tilt in the post-core-pulling stage and the initial stage of closing and resetting, thus causing unnecessary damage risk. Especially when closing the die, the slider is not restored smoothly, so that the slider is damaged or even damaged by bending. That's terrible. Correctly, the length of the slider in the sliding groove should not be less than 2/3 of the total length of the guide groove after the core pulling operation is completed. Only in this way can problems such as slider tilt be avoided. Many unpredictable problems can be avoided.
When designing and manufacturing moulds, they should be manufactured according to the requirements of the quality of plastic parts, the size of batches and the manufacturing period. In this way, it not only meets the requirements of products, but also is the simplest and most reliable in die structure, easy to process and low in cost. This kind of mold is relatively good. Once the die is generated, it will be useful and meet the basic performance requirements. There are many problems that may arise in injection moulds. It is necessary to prescribe remedies according to the symptoms, and use the correct methods to solve these problems according to the problems encountered. Extraordinary problems, the use of extraordinary solutions.